


LOW SPEED KNOCK
Low speed knock is generally caused by
- Worn U-joint.
- Worn side gear thrust washers.
- Worn pinion shaft bore.
DRIVELINE SNAP
A snap or clunk noise when the vehicle is shifted into gear (or the clutch engaged), can be caused by
- High engine idle speed.
- Transmission shift operation.
- Loose engine/transmission/transfer case mounts.
- Worn U-joints.
- Loose spring mounts.
- Loose pinion gear nut and companion flange.
- Excessive ring gear backlash.
- Excessive side gear to case clearance.
The source of a snap or a clunk noise can be determined with the assistance of a helper. Raise the vehicle on a hoist with the wheels free to rotate. Instruct the helper to shift the transmission into gear. Listen for the noise, a mechanics stethoscope is helpful in isolating the source of a noise.
| Condition | Possible Causes | Correction |
|---|---|---|
| Wheel Noise | 1. Wheel loose. | 1. Tighten loose nuts. |
| 2. Worn wheel bearing. | 2. Replace bearing. | |
| Axle Shaft Noise | 1. Damaged or worn axle shaft bearings and/or axle shaft journals. | 1. Replace axle shaft and/or axle shaft bearings. |
| 2. Bent or sprung axle shaft. | 2. Inspect and correct as necessary. | |
| Axle Shaft Broke | 1. Misaligned axle tube. | 1. Replace axle assembly. |
| 2 Vehicle overloaded. | 2. Replace broken shaft and avoid excessive weight on vehicle. | |
| 3. Erratic clutch operation. | 3. Replace broken shaft and avoid or correct erratic clutch operation. | |
| 4. Grabbing clutch. | 4. Replace broken shaft and inspect and repair clutch as necessary. | |
| Differential Cracked | 1. Improper adjustment of the differential bearings. | 1. Replace case and inspect gears and bearings for further damage. Set differential bearing pre-load properly. |
| 2. Excessive ring gear backlash. | 2. Replace case and inspect gears and bearings for further damage. Set ring gear backlash properly. | |
| 3. Vehicle overloaded. | 3. Replace case and inspect gears and bearings for further damage. Avoid excessive vehicle weight. | |
| 4. Erratic clutch operation. | 4. Replace case and inspect gears and bearings for further damage. Avoid erratic use of clutch. | |
| Differential Gears and/or Shims Scored or Galled | 1. Insufficient lubrication. | 1. Replace all damaged components. Fill differential with the correct fluid type and quantity. |
| 2. Improper grade of lubricant. | 2. Replace all damaged components. Fill differential with the correct fluid type and quantity. | |
| 3. Excessive spinning of one wheel/tire. | 3. Replace scored gears or differential assembly as necessary. Inspect all gears, pinion bores, and shaft for damage. Service as necessary. | |
| Loss Of Lubricant | 1. Lubricant level too high. | 1. Drain lubricant to the correct level. |
| 2. Worn axle shaft seals. | 2. Replace seals. | |
| 3. Cracked differential housing. | 3. Repair as necessary. | |
| 4. Worn pinion seal. | 4. Replace seal. Verify pinion bearing preload. | |
| 5. Worn/scored companion flange. | 5. Replace companion flange and seal. | |
| 6. Axle cover not properly sealed. | 6. Remove, clean and seal cover. | |
| Axle Overheating | 1. Lubricant level low. | 1. Fill differential to correct level. |
| 2. Improper grade of lubricant. | 2. Fill differential with the correct fluid type and quantity. | |
| 3. Bearing pre-loads too high. | 3. Adjust bearing pre-loads. | |
| 4. Insufficient ring gear backlash. | 4. Adjust ring gear backlash. | |
| Gear Teeth Broke | 1. Overloading. | 1. Replace gears. Examine other gears and bearings for possible damage. |
| 2. Erratic clutch operation. | 2. Replace gears and examine the remaining parts for damage. Avoid erratic clutch operation. | |
| 3. Ice-spotted pavement. | 3. Replace gears and examine remaining parts for damage. | |
| 4. Improper adjustments. | 4. Replace gears and examine remaining parts for damage. Ensure ring gear backlash is correct. | |
| Axle Noise | 1. Insufficient lubricant. | 1. Fill differential with the correct fluid type and quantity. |
| 2. Improper ring gear and pinion adjustment. | 2. Check ring gear and pinion contact pattern. Adjust backlash or pinion depth. | |
| 3. Unmatched ring gear and pinion. | 3. Replace gears with a matched ring gear and pinion. | |
| 4. Worn teeth on ring gear and pinion. | 4. Replace ring gear and pinion. | |
| 5. Loose pinion bearings. | 5. Replace pinion bearings, collapsible spacer, seal and pinion nut. | |
| 6. Loose differential bearings. | 6. Adjust differential bearing pre-load. | |
| 7. Ring gear run-out. | 7. Check ring gear and pinion contact pattern for tooth to tooth variation. Replace components as necessary. | |
| 8. Loose differential bearing cap bolts. | 8. Inspect differential components and replace as necessary. Ensure that the bearing caps are torqued to the proper specification. | |
| 9. Housing not machined properly. | 9. Replace housing. |
DIAGNOSTIC CHART
Scheme 374
Ring gear and pinion are supplied as matched sets. Identifying numbers for the ring gear and pinion are painted onto the pinion gear shank and the side of the ring gear. A plus (+) number, minus (-) number or zero (0) along with the gear set sequence number (2) (01 to 99) is on each gear. This first number is the amount (in thousandths of an inch) the depth varies (1) from the standard depth setting of a pinion marked with a (0). The next two numbers are the sequence number of the gear set. The standard depth provides the best teeth contact pattern.
Scheme 375
Compensation for pinion gear (5) depth variance is achieved with select shims (3). The shims are placed behind the rear pinion bearing cup (6).
If installing a new gear, note the depth variance number of the original and replacement pinion. Add or subtract this number from the original depth shim/oil slinger to compensate for the difference in the depth variances. The numbers represent thousands of an inch deviation from the standard. If the number is negative, add that value to the required thickness of the depth shims. If the number is positive, subtract that value from the thickness of the depth shim.
Pinion Gear Depth Variance Chart : Note where Old and New Pinion Marking columns intersect. Intersecting figure represents plus or minus the amount needed.
| Original Pinion Gear Depth Variance | Replacement Pinion Gear Depth Variance | |||||||||
|---|---|---|---|---|---|---|---|---|---|---|
| Α ^ , 4 | Α ^ , 3 | Α ^ , 2 | Α ^ , 1 | 0 | +1 | +2 | +3 | +4 | ||
| +4 | +0.008 | +0.007 | +0.006 | +0.005 | +0.004 | +0.003 | +0.002 | +0.001 | 0 | |
| +3 | +0.007 | +0.006 | +0.005 | +0.004 | +0.003 | +0.002 | +0.001 | 0 | Α ^ , 0.001 | |
| +2 | +0.006 | +0.005 | +0.004 | +0.003 | +0.002 | +0.001 | 0 | Α ^ , 0.001 | Α ^ , 0.002 | |
| +1 | +0.005 | +0.004 | +0.003 | +0.002 | +0.001 | 0 | Α ^ , 0.001 | Α ^ , 0.002 | Α ^ , 0.003 | |
| 0 | +0.004 | +0.003 | +0.002 | +0.001 | 0 | Α ^ , 0.001 | Α ^ , 0.002 | Α ^ , 0.003 | Α ^ , 0.004 | |
| Α ^ , 1 | +0.003 | +0.002 | +0.001 | 0 | Α ^ , 0.001 | Α ^ , 0.002 | Α ^ , 0.003 | Α ^ , 0.004 | Α ^ , 0.005 | |
| Α ^ , 2 | +0.002 | +0.001 | 0 | Α ^ , 0.001 | Α ^ , 0.002 | Α ^ , 0.003 | Α ^ , 0.004 | Α ^ , 0.005 | Α ^ , 0.006 | |
| Α ^ , 3 | +0.001 | 0 | Α ^ , 0.001 | Α ^ , 0.002 | Α ^ , 0.003 | Α ^ , 0.004 | Α ^ , 0.005 | Α ^ , 0.006 | Α ^ , 0.007 | |
| Α ^ , 4 | 0 | Α ^ , 0.001 | Α ^ , 0.002 | Α ^ , 0.003 | Α ^ , 0.004 | Α ^ , 0.005 | Α ^ , 0.006 | Α ^ , 0.007 | Α ^ , 0.008 | |
PINION GEAR DEPTH VARIANCE (EARLY BUILD)
Scheme 376

Ring gear and pinion are supplied as matched sets. Identifying numbers for the ring gear and pinion are laser etched onto the pinion gear shaft and the side of the ring gear. The first number (1) is the gear set sequence number and will be the same for the pinion and ring gear. The second line (2) has a plus (+) followed by a variance number. The third line (3) is the last six digits of the part number.
Compensation for pinion gear (5) depth variance is achieved with select shims (3). The shims are placed behind the rear pinion bearing cup (6).
Calculating the pinion depth variance will require some simple math. Subtract the number etched in the pinion from the standard pinion depth of 117.475 in millimeters.
Example 1: New pinion has a marking of 117.485. Subtract 117.485 from 117.475. (117.475 - 117.485 = negative (-) 0.010 mm).
Example 2: New pinion has a marking of 117.465. Subtract 117.465 from 117.475 (117.475 - 117.465 = positive (+) 0.010 mm).
This will indicate a positive (+) or negative (-) number and will be added or subtracted from the calculated shim thickness later in the procedure. Record the calculated pinion depth variance, positive (+) or negative (-), for later use.
Scheme 377

Measurements are taken with pinion bearing cups and pinion bearings installed in the housing. Take measurements with (special tool #C-3339A, Set, Dial Indicator) (1).
Scheme 378
Scheme 379
Scheme 380
Scheme 381

Scheme 382
Scheme 383
- Assemble (special tool #6739, Block, Height) (3), (special tool #8542, Gauge, Pinion Height) (6) and rear pinion bearing onto (special tool #6741, Screw) (5).
- Insert pinion block (1), pinion height block (2), rear bearing, and screw into the housing through pinion bearing cups.
- Install front pinion bearing and (special tool #6740, Cone) onto the screw. Tighten cone-nut until Torque To Rotate of the screw is 2.5 N.m (22 in. lbs.).
- Place (special tool #8541A, Set, Arbor Disc) (1) on (special tool #D-115-3, Arbor) (3) in position in the housing side bearing cradles. Install differential bearing caps on arbor discs and tighten cap bolts to 41 N.m (30 ft. lbs.).
- Assemble (special tool #C-3339A, Set, Dial Indicator) (3) into (special tool #D-115-2A, Block, Scooter) (2) and secure set screw.
- Place Scooter Block/Dial Indicator in position in axle housing so dial probe and scooter block are flush against the rearward surface of the pinion height block. Hold scooter block in place and zero the dial indicator. Tighten dial indicator face lock screw.
- Slide the dial indicator probe across the gap between the pinion height block and the arbor bar (1) with the scooter block against the pinion height block. Continue moving the dial probe to the crest of the arbor bar and record the highest reading. NOTE: Subtracting 0.072 mm (0.003) from the over all calculation is to compensate for the bearing growth factor.
- Selecting a shim for a pinion with painted markings: Select a shim equal to the dial indicator reading plus or minus the pinion depth variance number on the pinion gear then subtract 0.072 mm (0.003 in.) from the over all calculations. If the depth variance is -2, add 0.002 in. to the dial indicator reading. If the depth variance is +2, subtract 0.002 in. from the dial indicator reading.
- Selecting a shim for a pinion with laser etched markings: Select a shim equal to the dial indicator reading plus or minus the pinion depth variance calculated earlier, then subtract 0.072 mm (0.003 in.) from the over all calculations. If the calculated pinion depth variance recorded earlier is positive (+), add the calculated number from the dial indicator reading. If the calculated pinion depth variance recorded earlier is negative (-), subtract the calculated number to the dial indicator reading. NOTE: Shim thickness = Dial indicator reading plus (+) the pinion depth variance minus (-) the bearing growth factor. Example 1: Shim thickness = 1.90 mm (dial indicator reading) plus (+) +0.010 mm (a positive pinion depth variance) minus (-) 0.072 mm (bearing growth factor) = 1.838 mm. Example 2: Shim thickness = 1.90 mm (dial indicator reading) plus (+) - 0.010 mm (a negative pinion depth variance) minus (-) 0.072 mm (bearing growth factor) = 1.818 mm.
- Remove pinion head bearing cup from case and reinstall with selected shim as close as possible to the calculated number behind the bearing cup.
- Install a new collapsible spacer (1) on the pinion shaft.
- Lubricate rear pinion bearing with gear lube and install pinion gear into the housing.
- Apply Mopar® Thread Sealant to splines of the pinion shaft.
- Install companion flange with (special tool #C-3718, Installer, Flange) and (special tool #6719A, Holder, Yoke).
- Install bolts into two of the threaded holes in the companion flange 180° apart.
- Position (special tool #6719A, Holder, Yoke) (2) against the companion flange and install a bolt and washer into one of the remaining threaded holes. Tighten the bolts so the (special tool #6719A, Holder, Yoke) is held to the flange.
- Install new pinion nut.
- Hold companion flange with (special tool #6719A, Holder, Yoke) (2) and tighten pinion nut with a torque wrench (3) to 285 N.m (210 ft. lbs.). NOTE: Do not exceed minimum torque 285 N.m (210 ft. lbs.) at this point.
- Rotate pinion several times to seat pinion bearings.
- Measure pinion torque to rotate (1) with an inch pound torque wrench (2). Measure pinion rotating torque frequently to avoid over-crushing the collapsible spacer. Pinion Torque To Rotate is: Original Bearings: 1 - 1.7 N.m (10 - 15 in. lbs.) New Bearings: 1.9 - 2.5 N.m (17 - 22 in. lbs.) NOTE: If pinion torque to rotate is low, tighten pinion nut in 6.8 N.m (5 ft. lbs.) increments until pinion torque to rotate is achieved.
| CAUTION | Never loosen pinion nut to decrease pinion bearing rotating torque. If pinion torque to rotating is exceeded a new collapsible spacer must be installed. Failure to follow these instruction will damage the axle. |
Scheme 384
Scheme 385
Scheme 386
Scheme 387
- Before installing differential, use a 12 inch caliper to measure between the inner most part of the holes (1 and 2) and record reading for later use.
- Install the differential and bearing caps and tighten to 14 N.m (10 ft. lbs.) to retain cups while adjusting.
- Turn both thread adjusters inward with (special tool #C-4164, Wrench, Differential Preload) until differential bearing end-play is eliminated and ring gear backlash is approximately 0.025 mm (0.001 in.). Seat bearing cups by rapidly rotating the pinion gear a half turn back and forth several times.
- Install dial indicator (1) with plunger position against drive side of a ring gear tooth. Measure and record backlash at 4 positions, 90 degrees apart around the ring gear. Mark lowest backlash position on the ring gear and make all backlash measurements at this location.
- Loosen left-side adjuster and tighten right-side threaded adjuster with (special tool #C-4164, Wrench, Differential Preload) (3) to obtain a backlash of 0.076 - 0.102 mm (0.003 - 0.004 in.).
- Tighten both adjusters to 14 N.m (10 ft. lbs.). Seat differential bearing cups by rapidly rotating the pinion gear a half turn back and forth several times.
- Tighten differential bearing cap bolts 136 N.m (100 ft. lbs.).
- Tighten right-side threaded adjuster to 102 N.m (75 ft. lbs.). Seat differential bearing cups by rapidly rotating the pinion gear a half turn back and forth several times. Continue this procedure until right-side adjuster torque remains a constant 102 N.m (75 ft. lbs.).
- Measure the ring gear backlash. Backlash should be 0.12 - 0.20 mm (0.005 - 0.008 in.). If backlash is less than 0.12 mm (0.005 in.) increase the torque on the right-side threaded adjuster until specified backlash is obtained. If backlash is more than 0.20 mm (0.008 in.) repeat procedure from the beginning.
- Tighten left-side threaded adjuster to 102 N.m (75 ft. lbs.). Seat differential bearing cups by rapidly rotating the pinion gear a half turn back and forth several times. Continue this procedure until left-side adjuster torque remains a constant 102 N.m (75 ft. lbs.).
- Use a 12 inch caliper to measure between the inner most part of the holes (1 and 2) and compare between reading recorded in earlier step.
- Subtract first reading from the second reading. Case spread should have increased between 0.050 mm (0.002 in) and 0.100 mm (0.004 in). If below 0.050 mm (0.002 in), increase torque evenly on both threaded adjusters and recheck backlash. If above 0.100 mm (0.004 in), decrease torque evenly on both threaded adjusters and recheck backlash.
- Install threaded adjuster locks and tighten the lock screws to 11 N.m (97 in. lbs.).
- Measure backlash at 4 positions, 90 degrees apart around the ring gear. Maximum ring gear backlash variation is 0.076 mm (0.003 in.).
Scheme 388
- Wipe clean each tooth of the ring gear.
- Apply gear marking compound to all of the ring gear teeth.
- Verify bearing cap bolts are torque to specification.
- Apply parking brakes lightly to create at 14 N.m (10 ft. lbs.) pinion rotating torque. NOTE: If the axle is not in the vehicle, a large screwdriver can be used between the outer smooth edge of the ring gear and the axle housing to provide resistance.
- Rotate the pinion/pinion flange 4 full revolutions in each directions.
- Read gear tooth contact pattern.
Gear contact pattern is correct. Backlash and pinion depth is correct.
Scheme 389
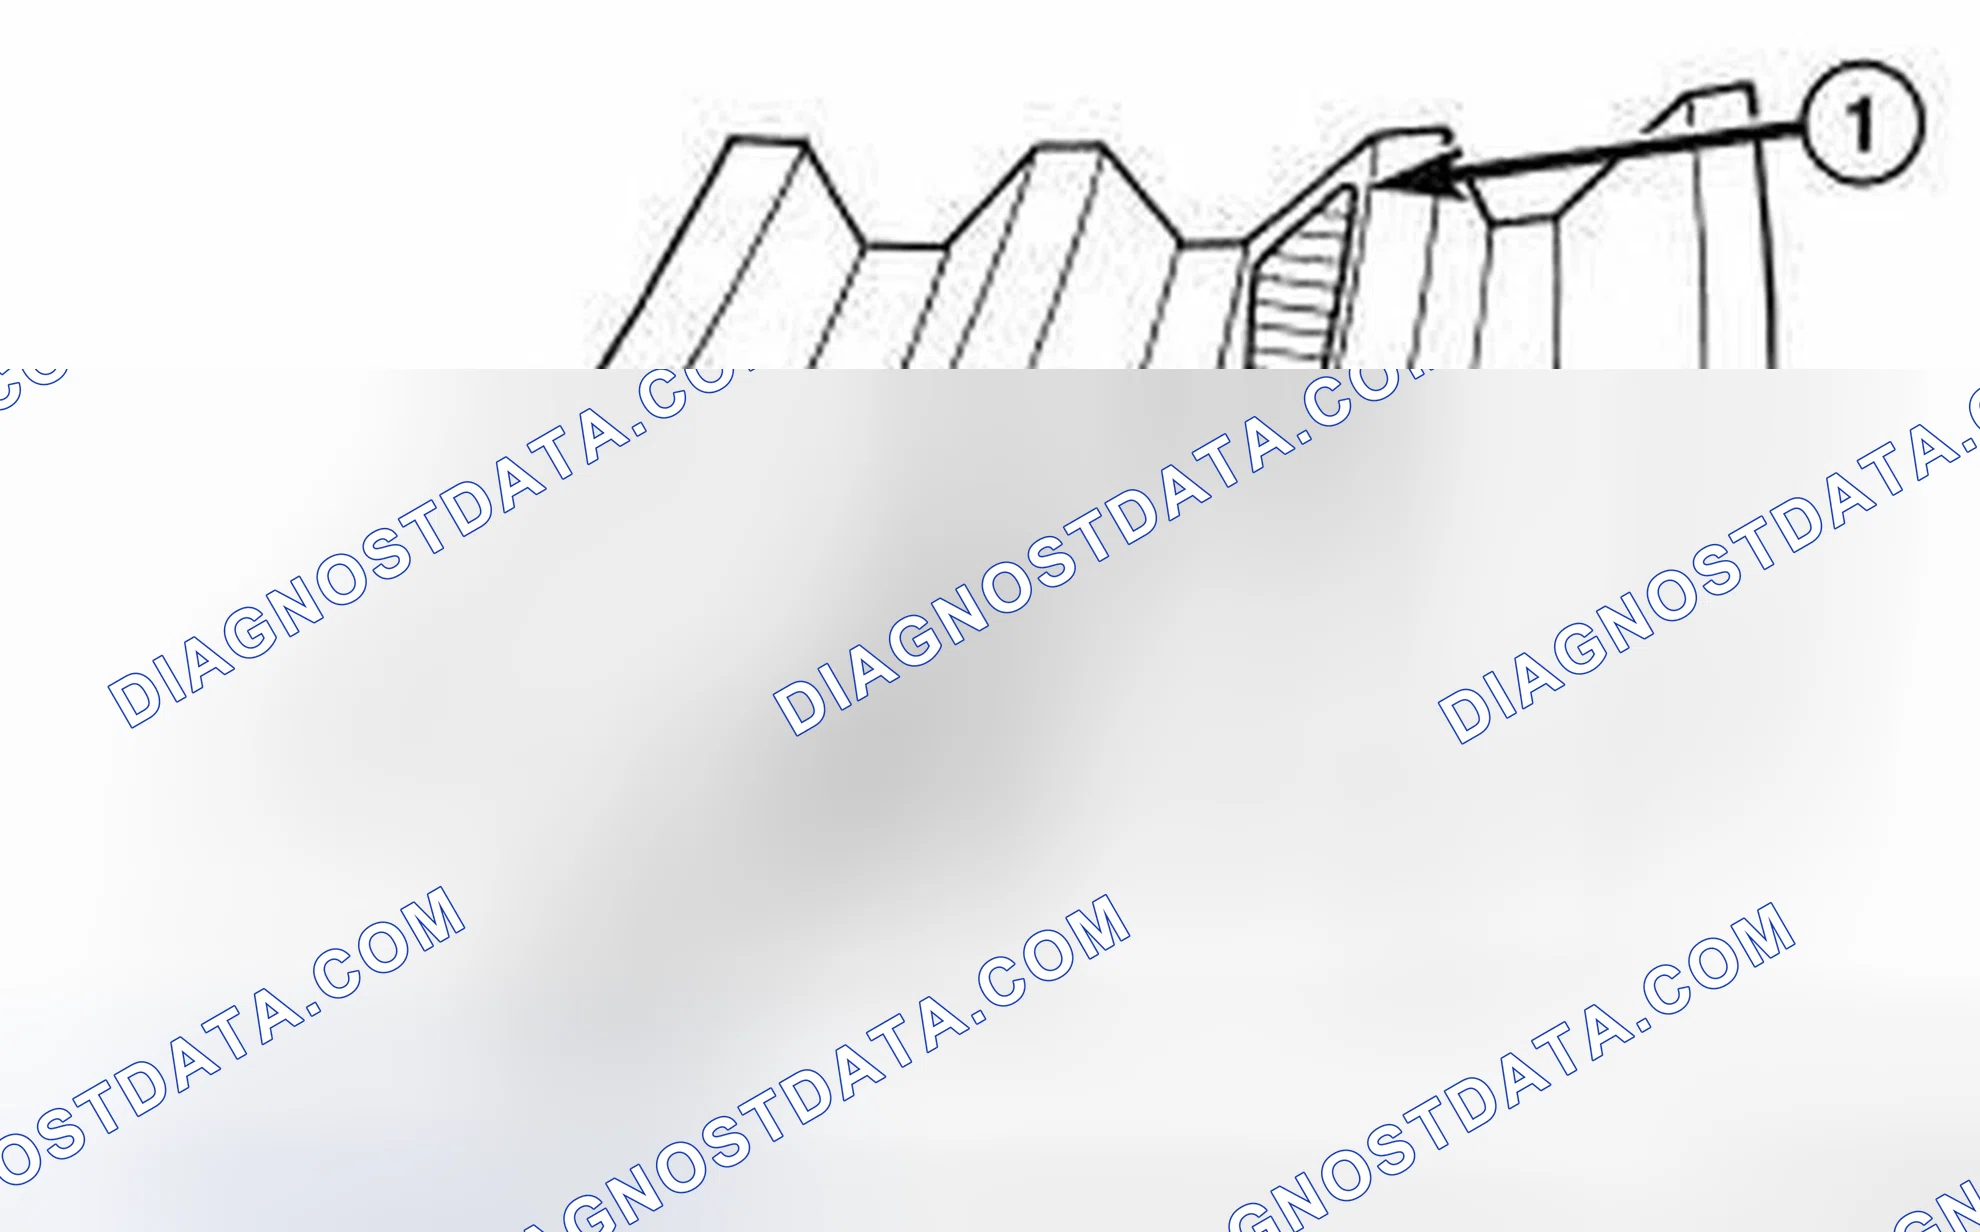
Ring gear too far away from pinion gear, coast side toe (1) and drive side heel (2). Decrease backlash, by moving the ring closer to the pinion gear using the adjusters.
Scheme 390
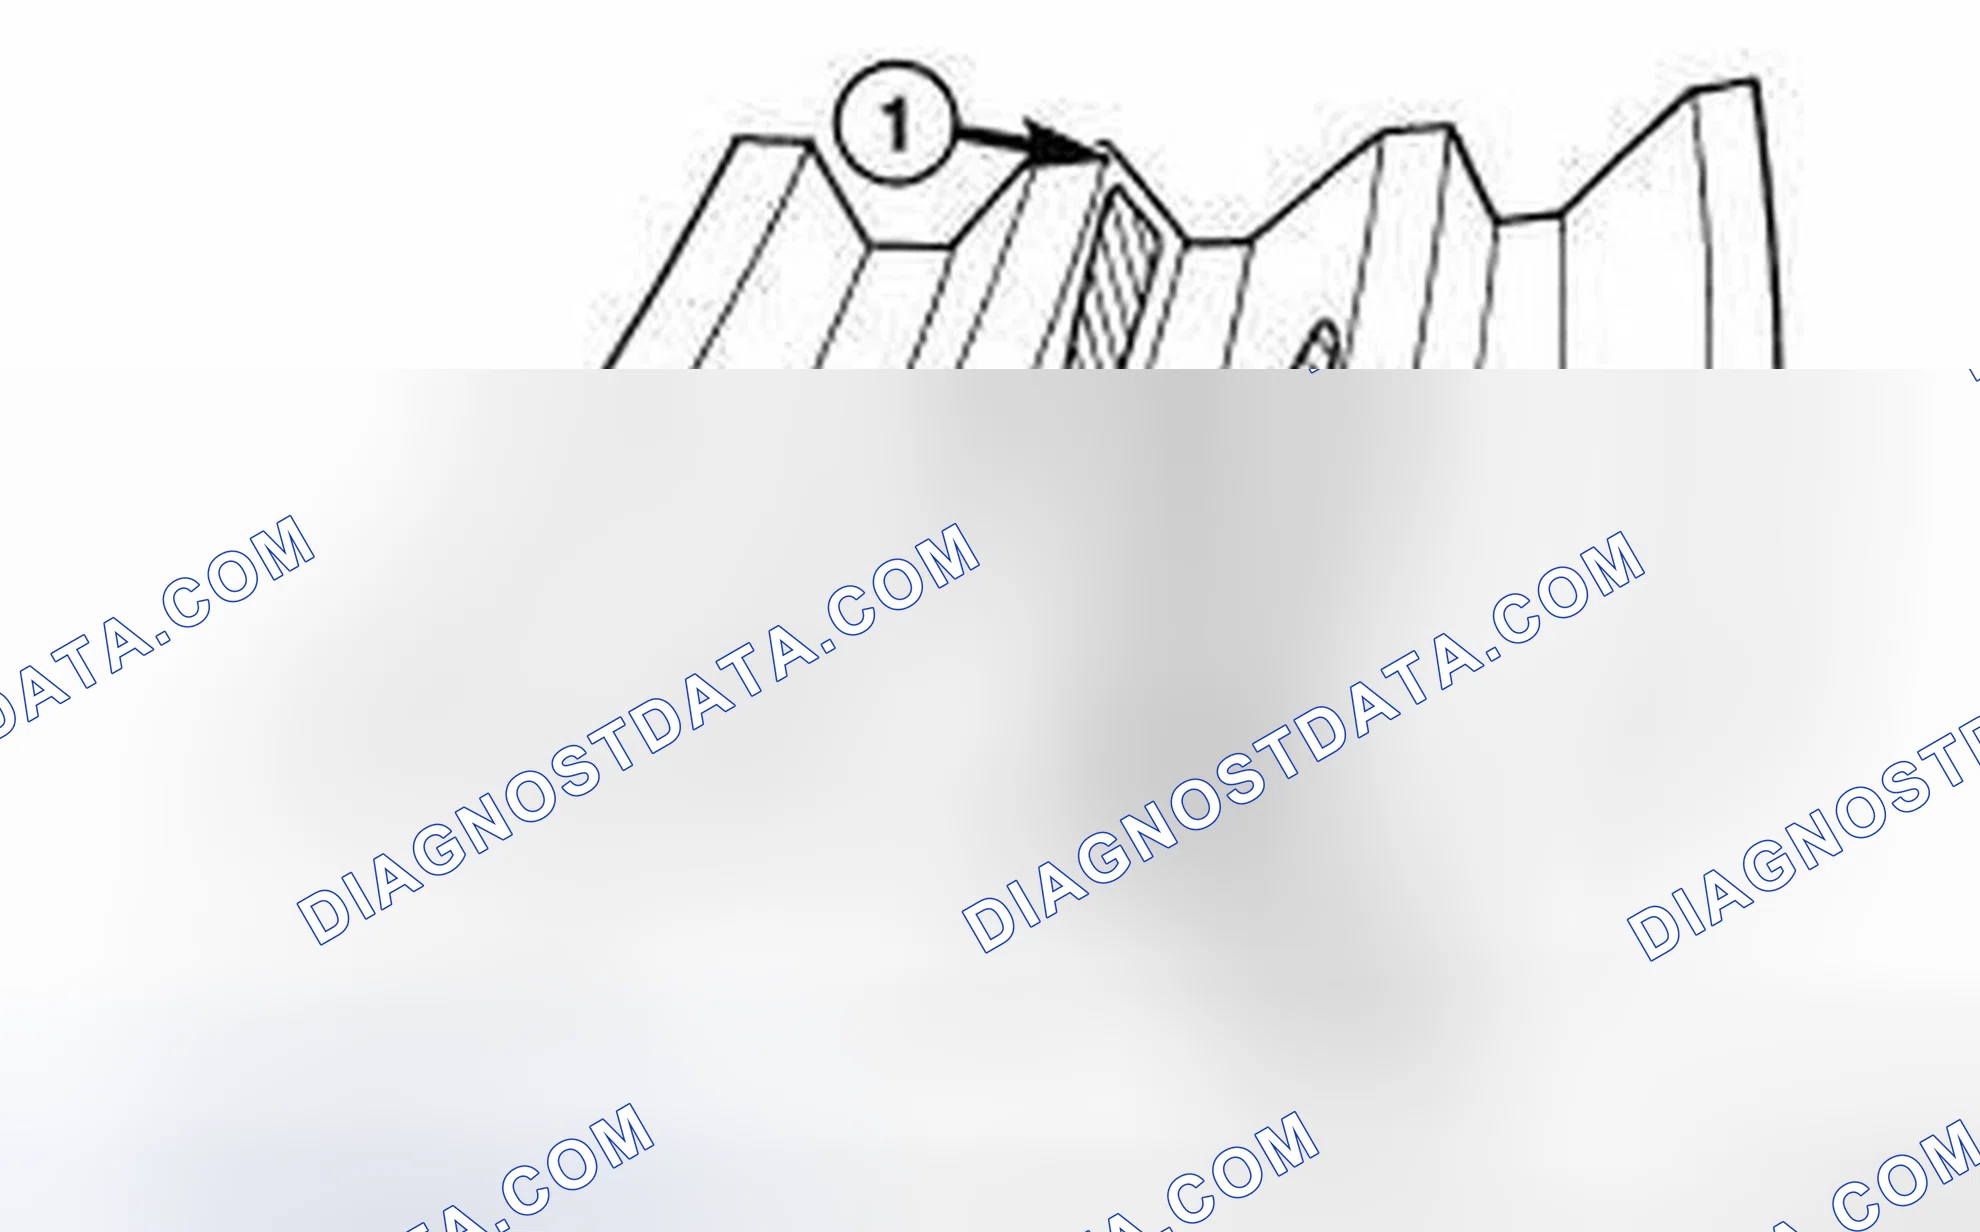
Ring gear too close to pinion gear, drive side toe (1) and coast side heel (2). Increase backlash, by moving the ring away from the pinion gear using the adjusters.
Scheme 391
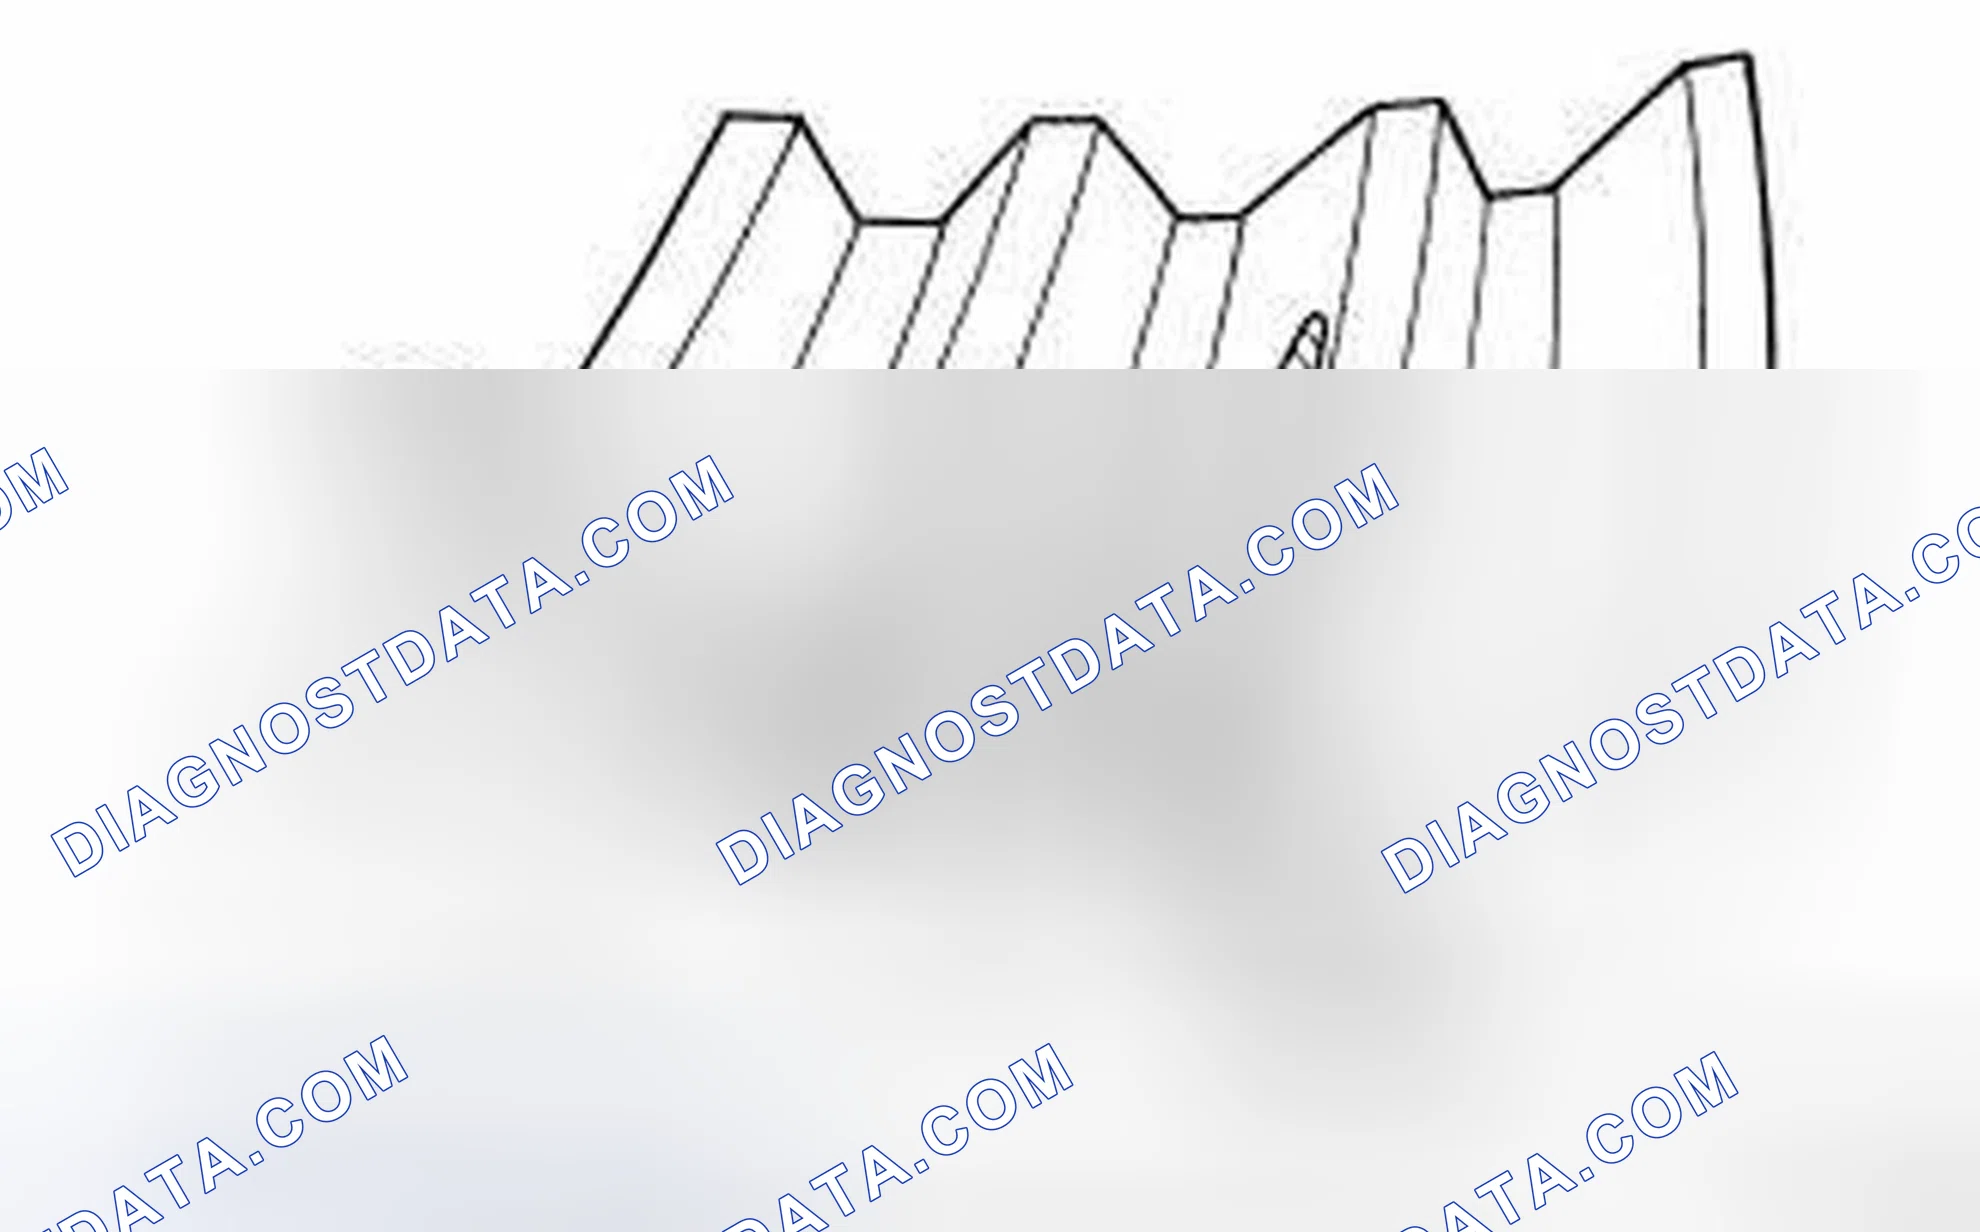
Ring gear too far away from pinion gear, drive side heel (1) and coast side heel (2). Decrease backlash, by moving the ring closer to the pinion gear using the adjusters.
Scheme 392
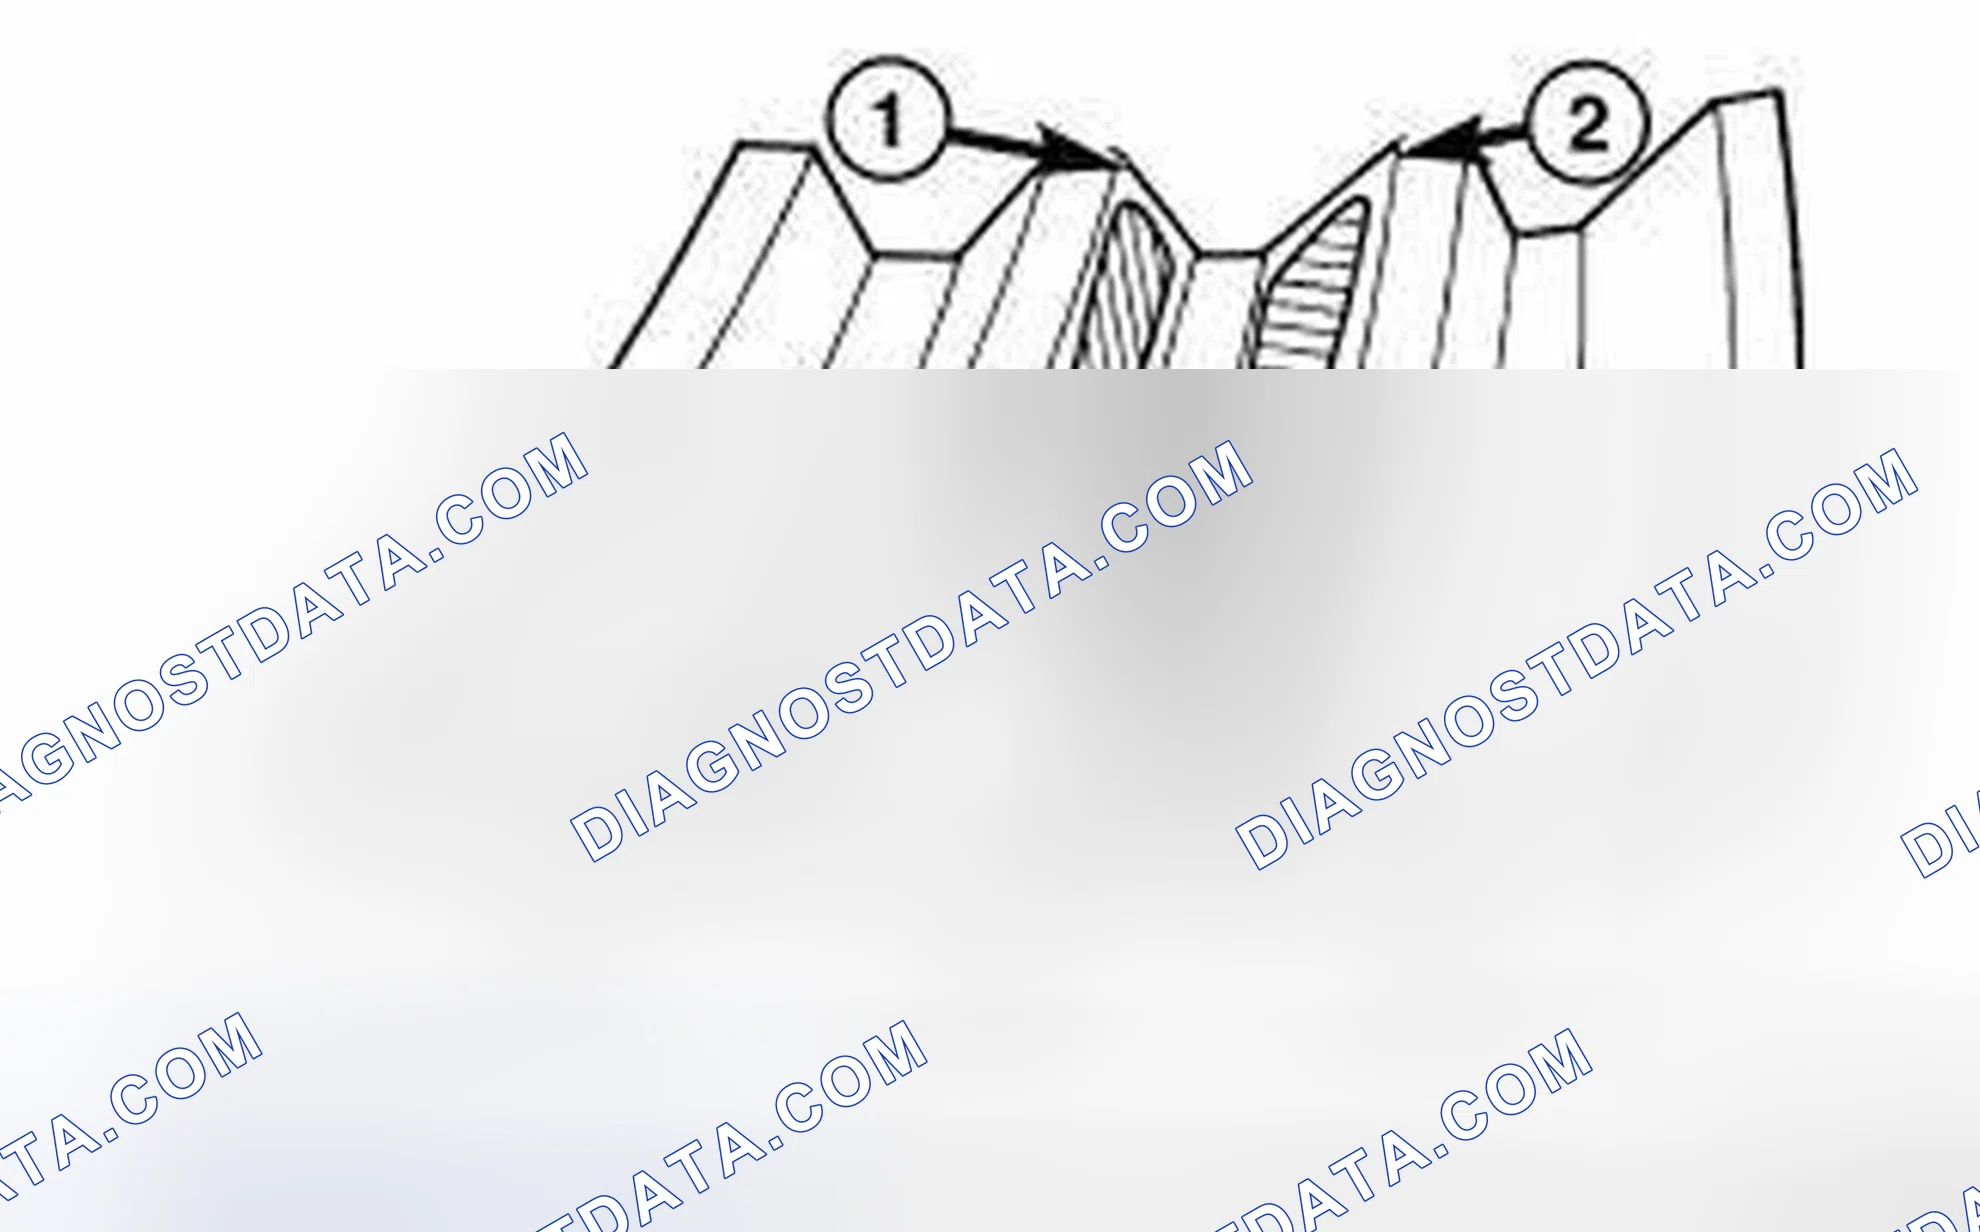
Ring gear too close to pinion gear, drive side toe (1) and coast side toe (2). Increase backlash, by moving the ring away from the pinion gear using the adjusters.
Scheme 393
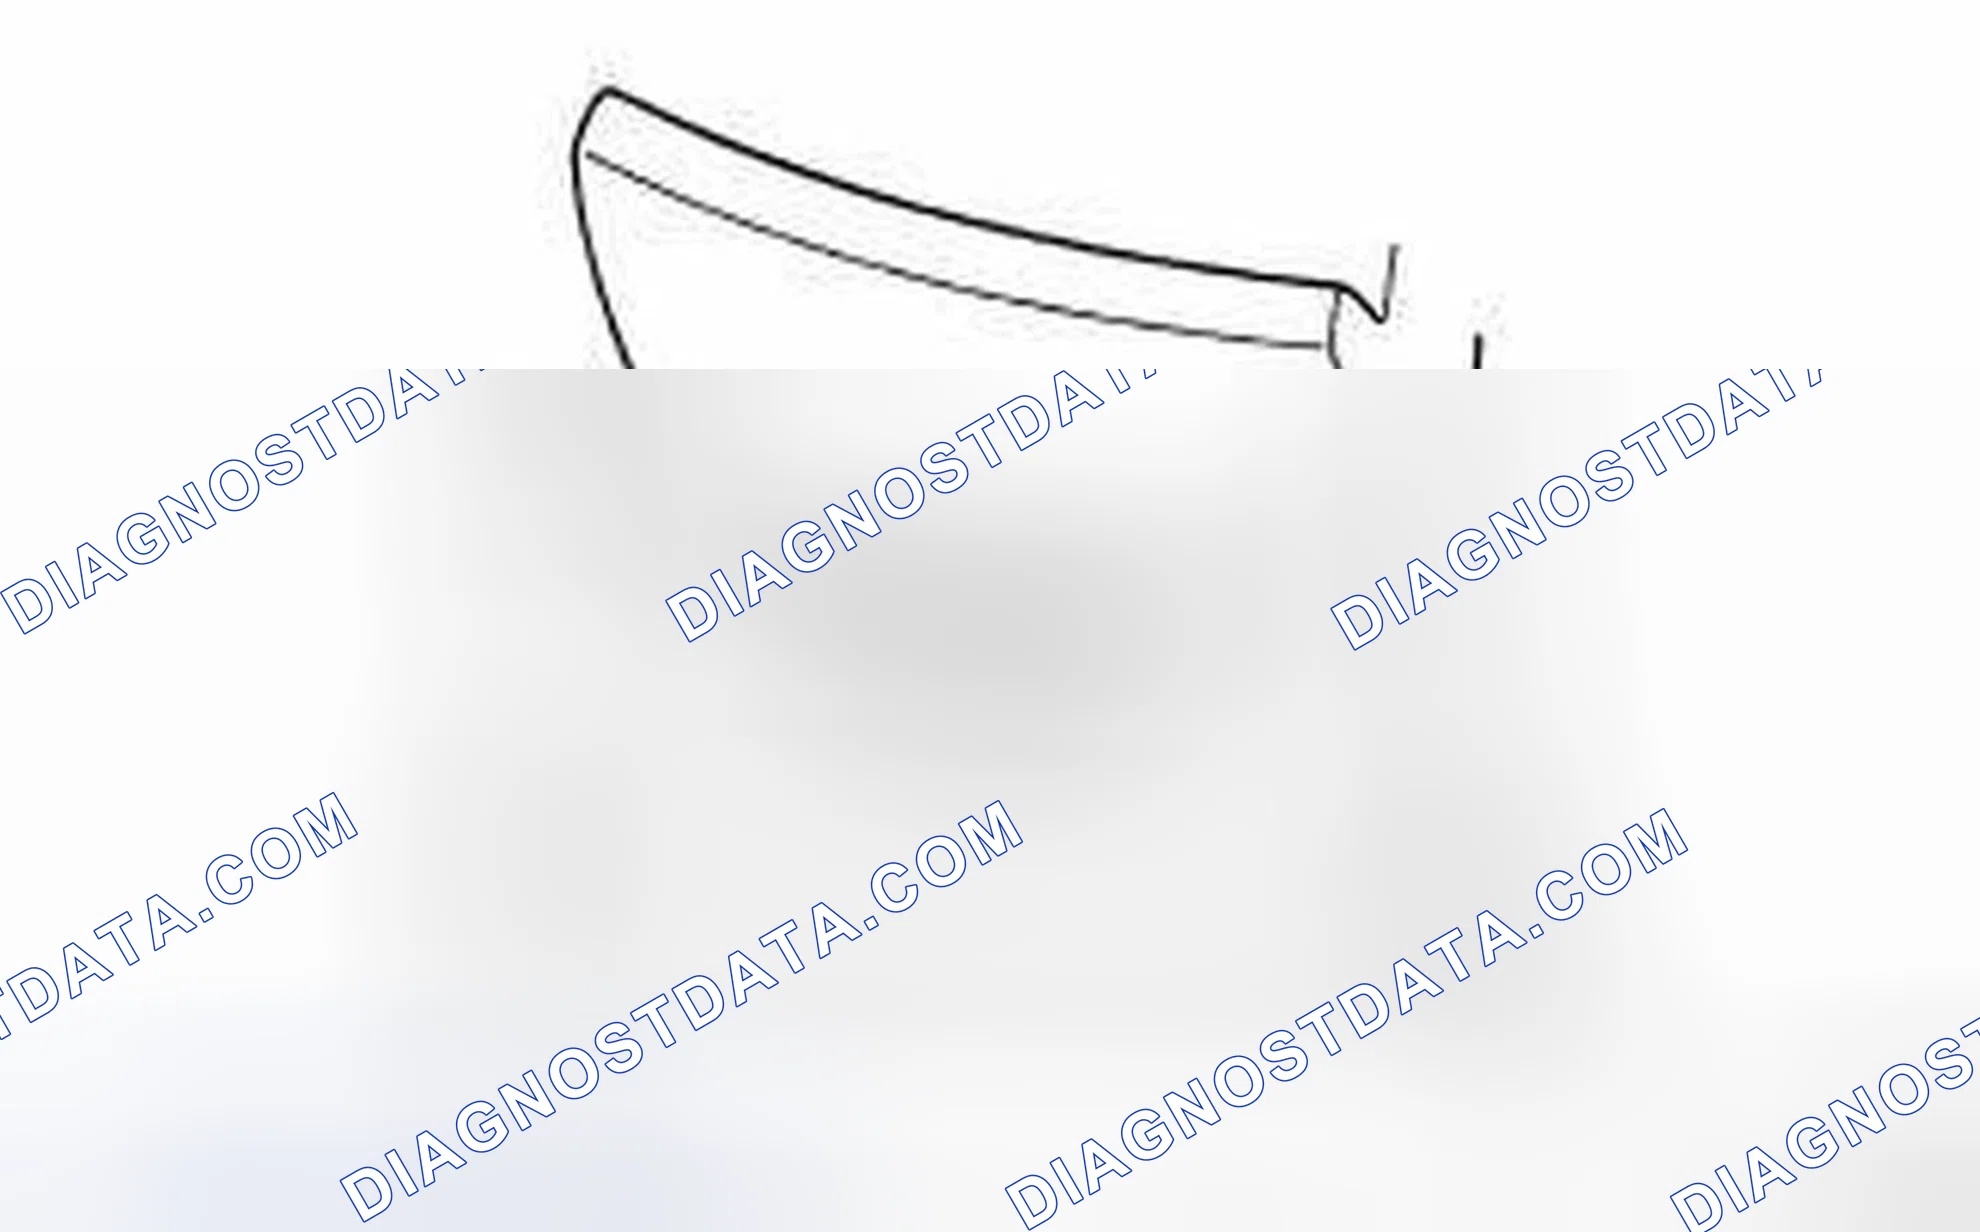
Pinion gear set too far from the ring gear. Decrease pinion gear distance, by increasing the pinion depth shim thickness.
Scheme 394
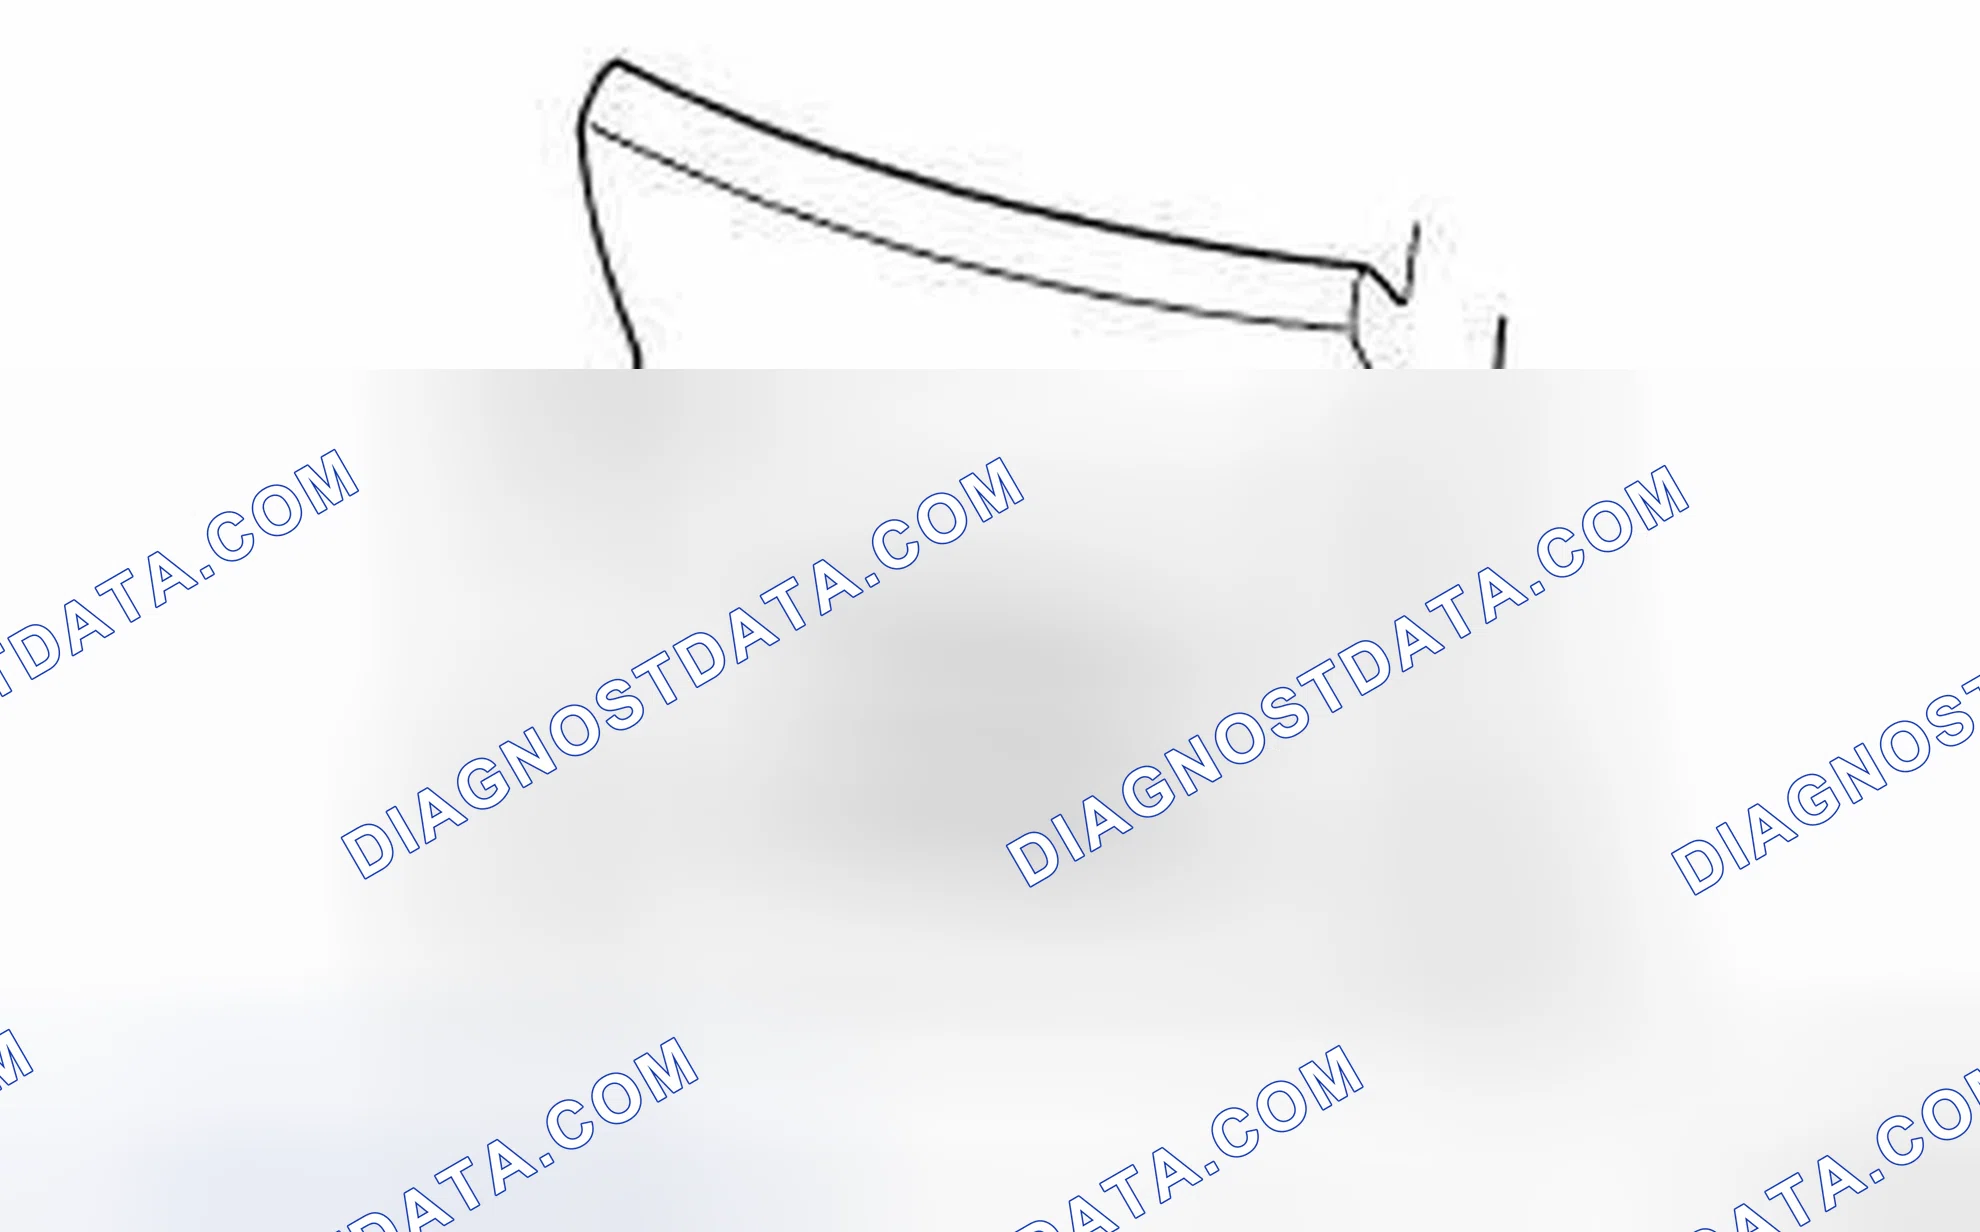
Pinion gear set too close to the ring gear. Increase pinion distance, by decreasing the pinion depth shim thickness.
Note. It may be necessary to adjust the backlash after adjusting the pinion distance.
SIDE GEAR CLEARANCE (OPEN DIFFERENTIALS)
Visually inspect differential case, pinion mate shaft, axle shaft end button, C-lock, differential pinion gears, differential side gears and washers for damage or excessive wear. Replace damaged components.
- Assemble differential and install.
- Install differential pinion mate shaft locking screw and hand tighten to locate the shaft.
- Mount dial indicator base on the axle tube flange.
- Push axle shaft inward until its end touches differential pinion mate shaft. Set dial indicator plunger on the end of axle shaft flange surface and zero dial indicator.
- Pull axle shaft out until it stops and record dial indicator end-play reading. Rotate axle shaft about 180 degrees and record dial indicator end-play reading again. Two readings should be within 0.05 mm (0.002 in.).
- Conduct the same procedure on the axle shaft on the opposite side.
End-play specification should be 0.13 mm - 0.38 mm (0.005 - 0.015 in.). If specification can not be met, shim side gears and/or replace differential case.